MS factory Upgrades Pharmaceutical Filter Production Facilities
Why This Upgrade Matters
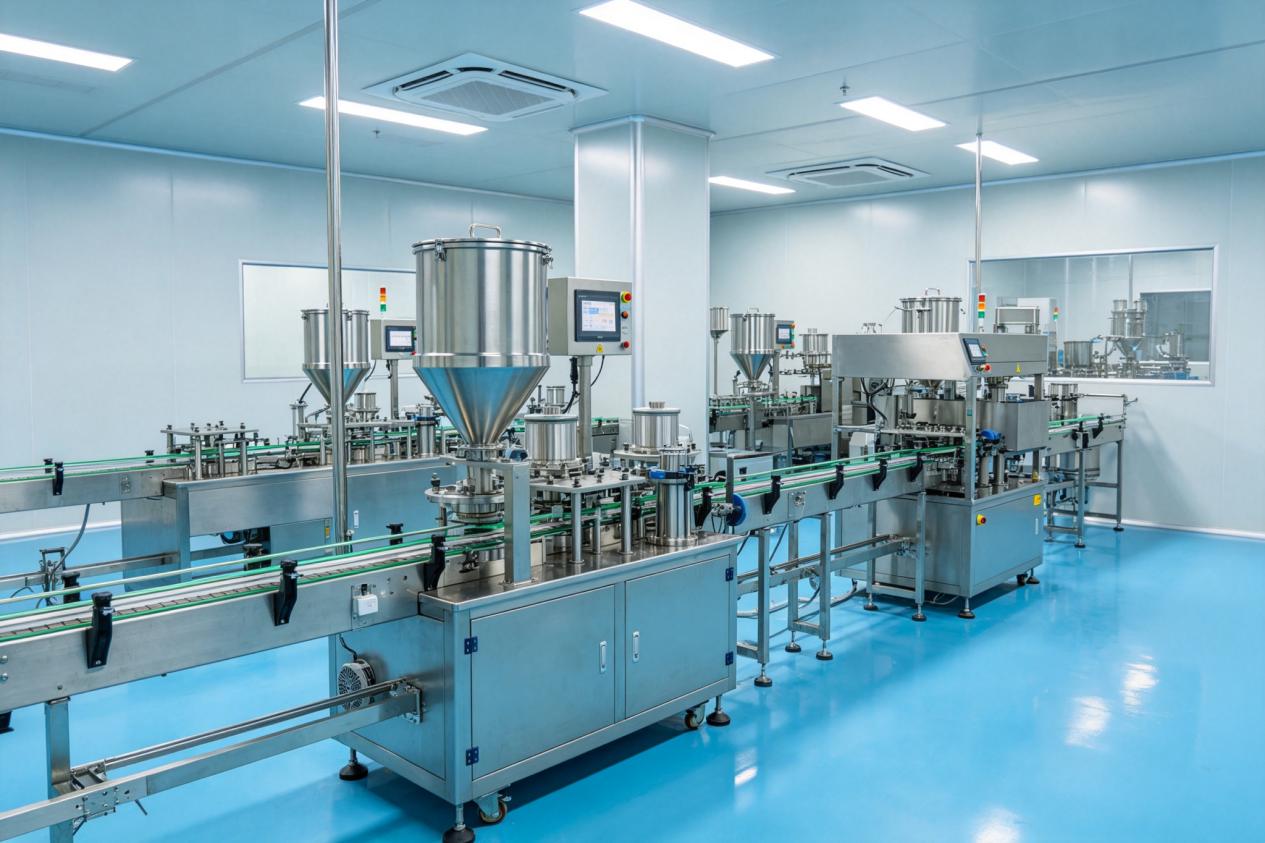
Pharmaceutical and biopharmaceutical manufacturers increasingly demand filtration products that deliver consistent batch quality, comprehensive documentation, and reliable regulatory compliance. To meet these expectations, MS factory has completed a significant upgrade of its pharmaceutical filter production infrastructure. The upgraded facility integrates enhanced environmental controls, automated membrane pleating and assembly equipment, and expanded integrity testing capacity, all aimed at improving product consistency and production reliability.
This upgrade reflects MS factory's ongoing commitment to serving the global biopharmaceutical market, where filtration is not a commodity but a critical process component that directly impacts product sterility, yield, and regulatory standing. By investing in production infrastructure, the company is better positioned to support both standard catalog products and custom OEM configurations for pharmaceutical equipment manufacturers and system integrators worldwide.
Production Capabilities Now Available
The upgraded facility supports manufacturing across several key pharmaceutical filtration product lines. For sterile air and solvent applications, the ePTFE Capsule Filter line is produced with enhanced membrane pleating controls that improve pleat uniformity and structural consistency across production runs. The naturally hydrophobic expanded PTFE membrane delivers broad chemical resistance and reliable microbial retention, with each unit undergoing integrity verification before release.
For sterilization-in-place and cleaning-in-place applications, the SIP/CIP Capsule Filter line benefits from upgraded housing molding and thermal bonding equipment that strengthens seal integrity through repeated thermal cycles. The facility also produces the PVDF Capsule Filter line for biological product filtration, where low protein binding and hydrophilic wettability are important, as well as the Vent Filter series for sterile tank venting in pharmaceutical, biotech, and food and beverage manufacturing.
Quality Controls Built Into Every Batch
Quality assurance is embedded throughout the upgraded production process. The facility includes a dedicated integrity testing laboratory equipped with automated bubble point and diffusion test systems, enabling 100 percent integrity testing for all sterilizing-grade products. Beyond integrity testing, each filter undergoes dimensional inspection, pressure verification, and visual examination before shipment, with all results recorded against unique batch identifiers for complete traceability.
Materials of construction meet USP Class VI 121°C biocompatibility requirements for plastics, and products manufactured in the facility comply with FDA 21 CFR food contact regulations and EU 10/2011 directives for applicable applications. Material compliance statements, batch traceability records, and inspection reports are available to support customer qualification files and regulatory submissions. The production environment itself is monitored for particulate and microbial contamination on a regular schedule, with environmental monitoring records maintained for audit purposes.
Customization and OEM Partnership Options
The upgraded production infrastructure enables MS factory to offer flexible customization and OEM support for pharmaceutical equipment manufacturers. Available customization options include membrane grade selection, pore size configuration, filtration area, capsule dimensions, vent port design, connection style, and packaging solutions. For original equipment manufacturers, the company provides dimensional drawings, flow performance data, chemical compatibility guidance, and private label branding options to support integration into finished systems.
The engineering team collaborates directly with customers to develop tailored filtration solutions for specific process requirements, whether the application involves sterile air filtration for fermenters, tank venting for WFI storage, solvent filtration for API production, or high-flow prefiltration for reverse osmosis systems. This collaborative approach ensures that each filtration solution is optimized for the specific operating conditions, flow requirements, and regulatory expectations of the customer's process.
What This Means for Your Procurement
The upgraded production facility is fully operational and accepting orders for both standard products and custom configurations. Pharmaceutical and biopharmaceutical buyers can expect improved production consistency, more reliable lead times, expanded customization options, and comprehensive documentation support with every order. Whether the requirement is standard catalog capsule filters for routine production or custom-configured filtration solutions for specialized equipment, MS factory can deliver reliable, high-quality products backed by complete documentation and responsive technical support.
By combining in-house membrane production, automated capsule assembly, comprehensive quality testing, and direct engineering support, MS factory serves as a dependable sourcing partner for pharmaceutical and biopharmaceutical manufacturers seeking reliable, cost-effective, and compliant filtration solutions. To discuss specific filtration requirements, request a formal quotation, or learn more about the upgraded production capabilities and available documentation packages, reach out to the MS factory sales team at your convenience.
Previous:No News